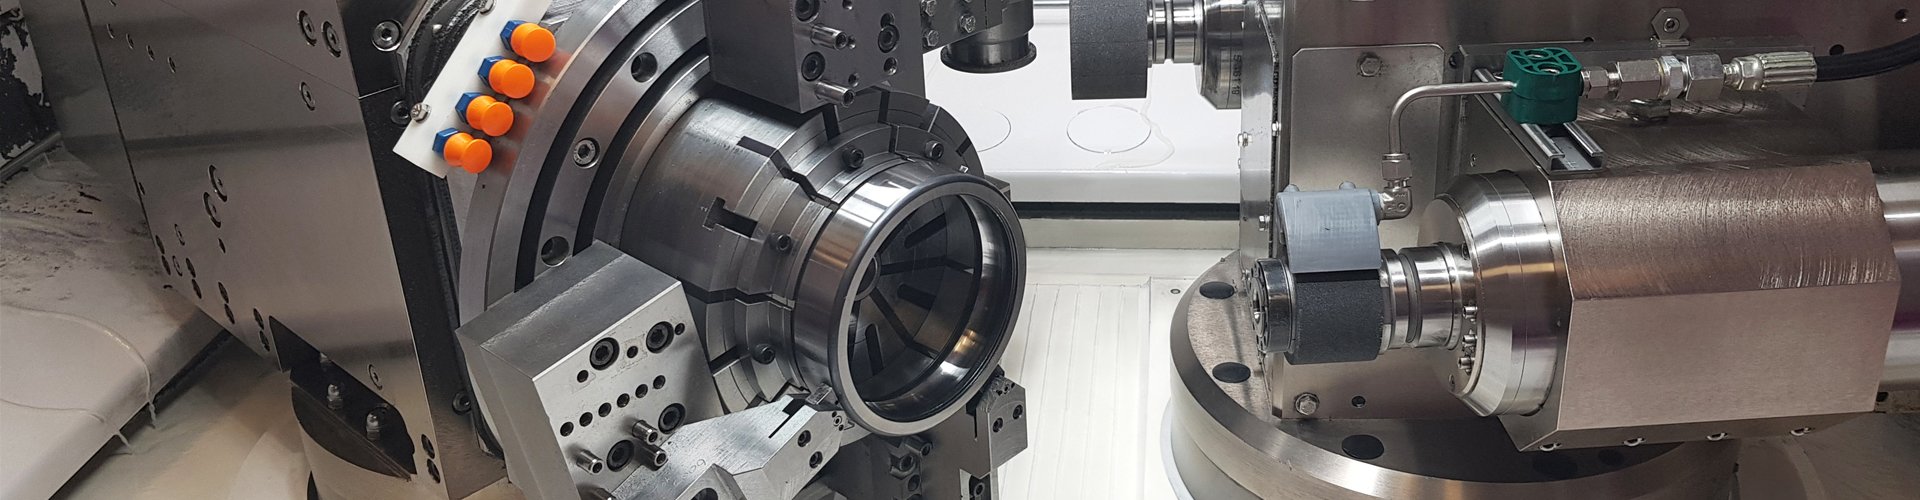
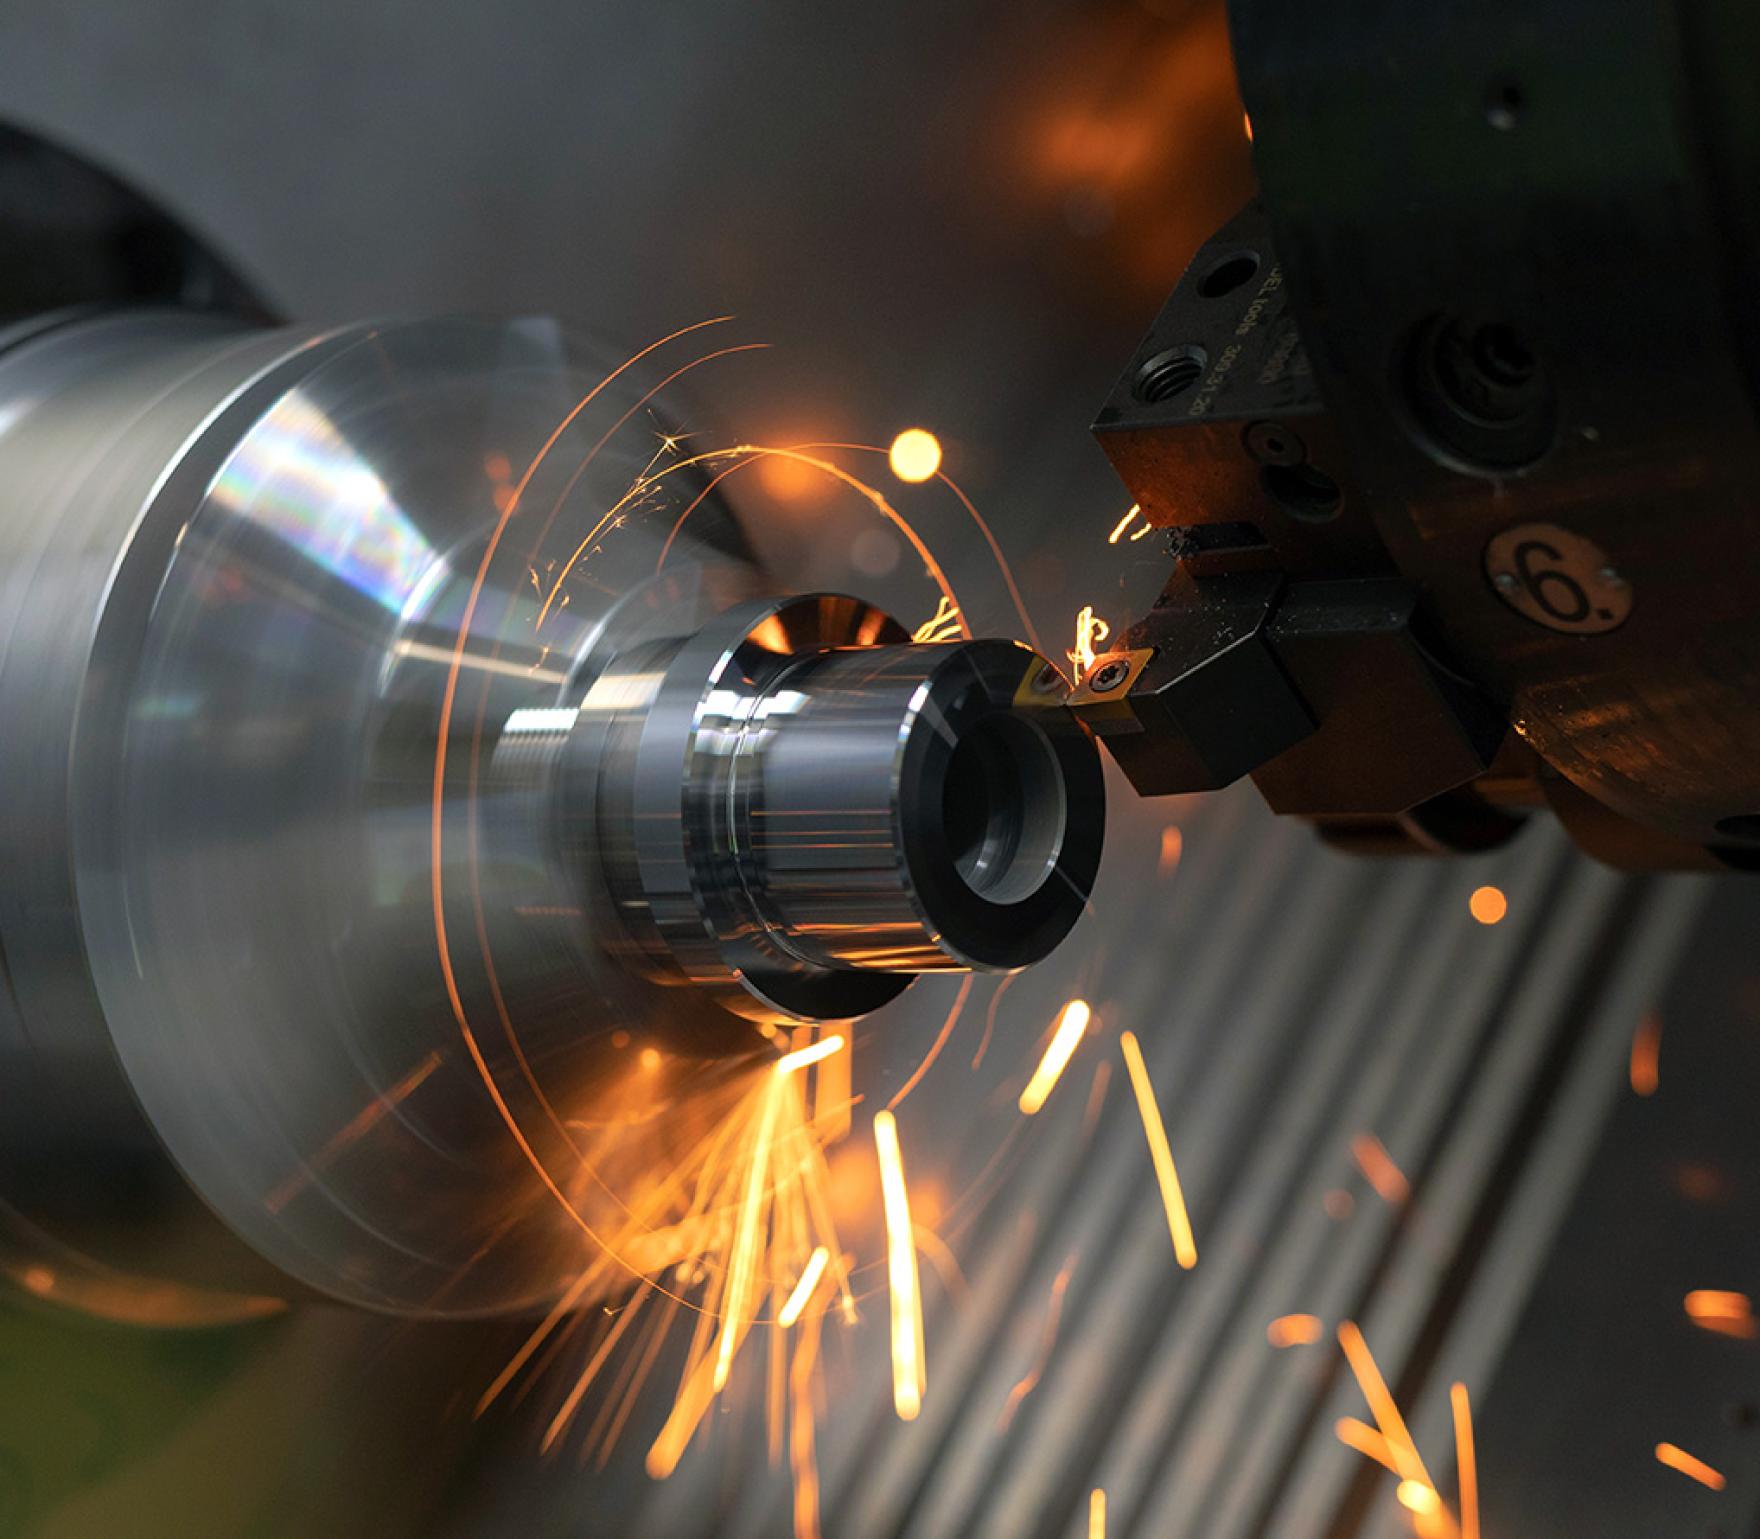
Controlled in one plant
Ring turning, heat treatment, grinding and final inspection run in the same facility — every accuracy class traceable to the same line.
The process, end to end
CNC turning & grinding
Ring turning, rib and raceway grinding, super finishing on dedicated lines.
Heat treatment
Through hardening with controlled cooling and dimensional stabilization.
Assembly & sealing
Cage fitting, seal mounting and metered grease filling for hub unit assemblies.
Metrology & packing
Roundness, vibration and geometry measured on every accuracy class before packing.
Inside the plant
Profiles and raceway channels turned in one clamping on dedicated CNC lines.
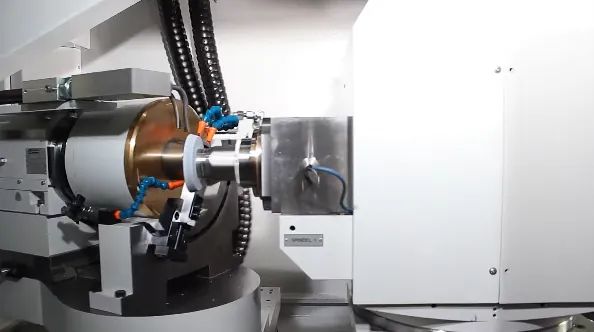
Inner-ring rib grinding machines tooled up for batch-to-batch consistency.
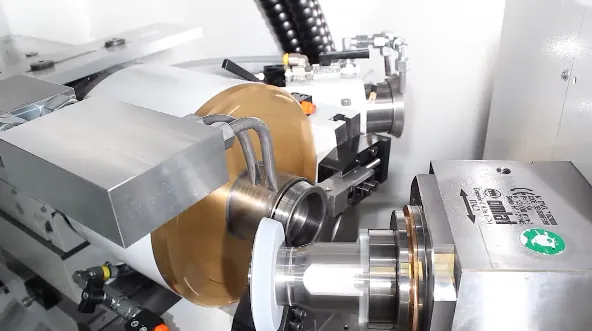
Wheel dressing and rib finishing hold geometry at micron level.
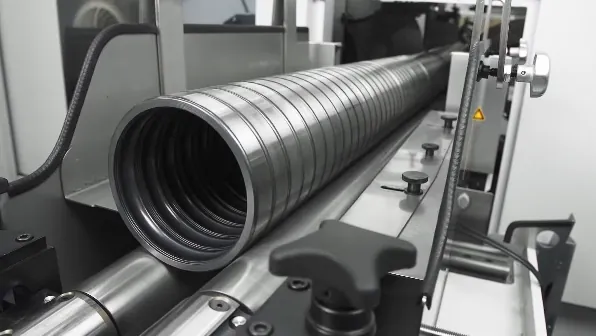
Ground outer rings queued for super finishing and final inspection.
Quality control on every unit
- ✓100% geometry and roundness inspection before packing
- ✓Vibration and noise tested on every accuracy class
- ✓End play and preload torque set at factory for hub units
- ✓Full material traceability from ring to finished unit
- ✓Metrology lab: roundness, vibration and geometry measured per batch
- ✓Optimized rib geometry for lower frictional heating
Lead times
| Standard models | 3 days |
|---|---|
| Production orders | 10 – 25 days |
| Custom tooling | 25 days |
| Matched sets / pre-adjusted | On request |
| Packing | Single box · OEM branding on request |
Audit our process
Ask for the production flow of your specific model — we share process parameters, inspection records and test data with serious buyers.
- ✓Process and inspection records on request
- ✓Sample runs before volume orders
- ✓Factory visits and video audits welcome